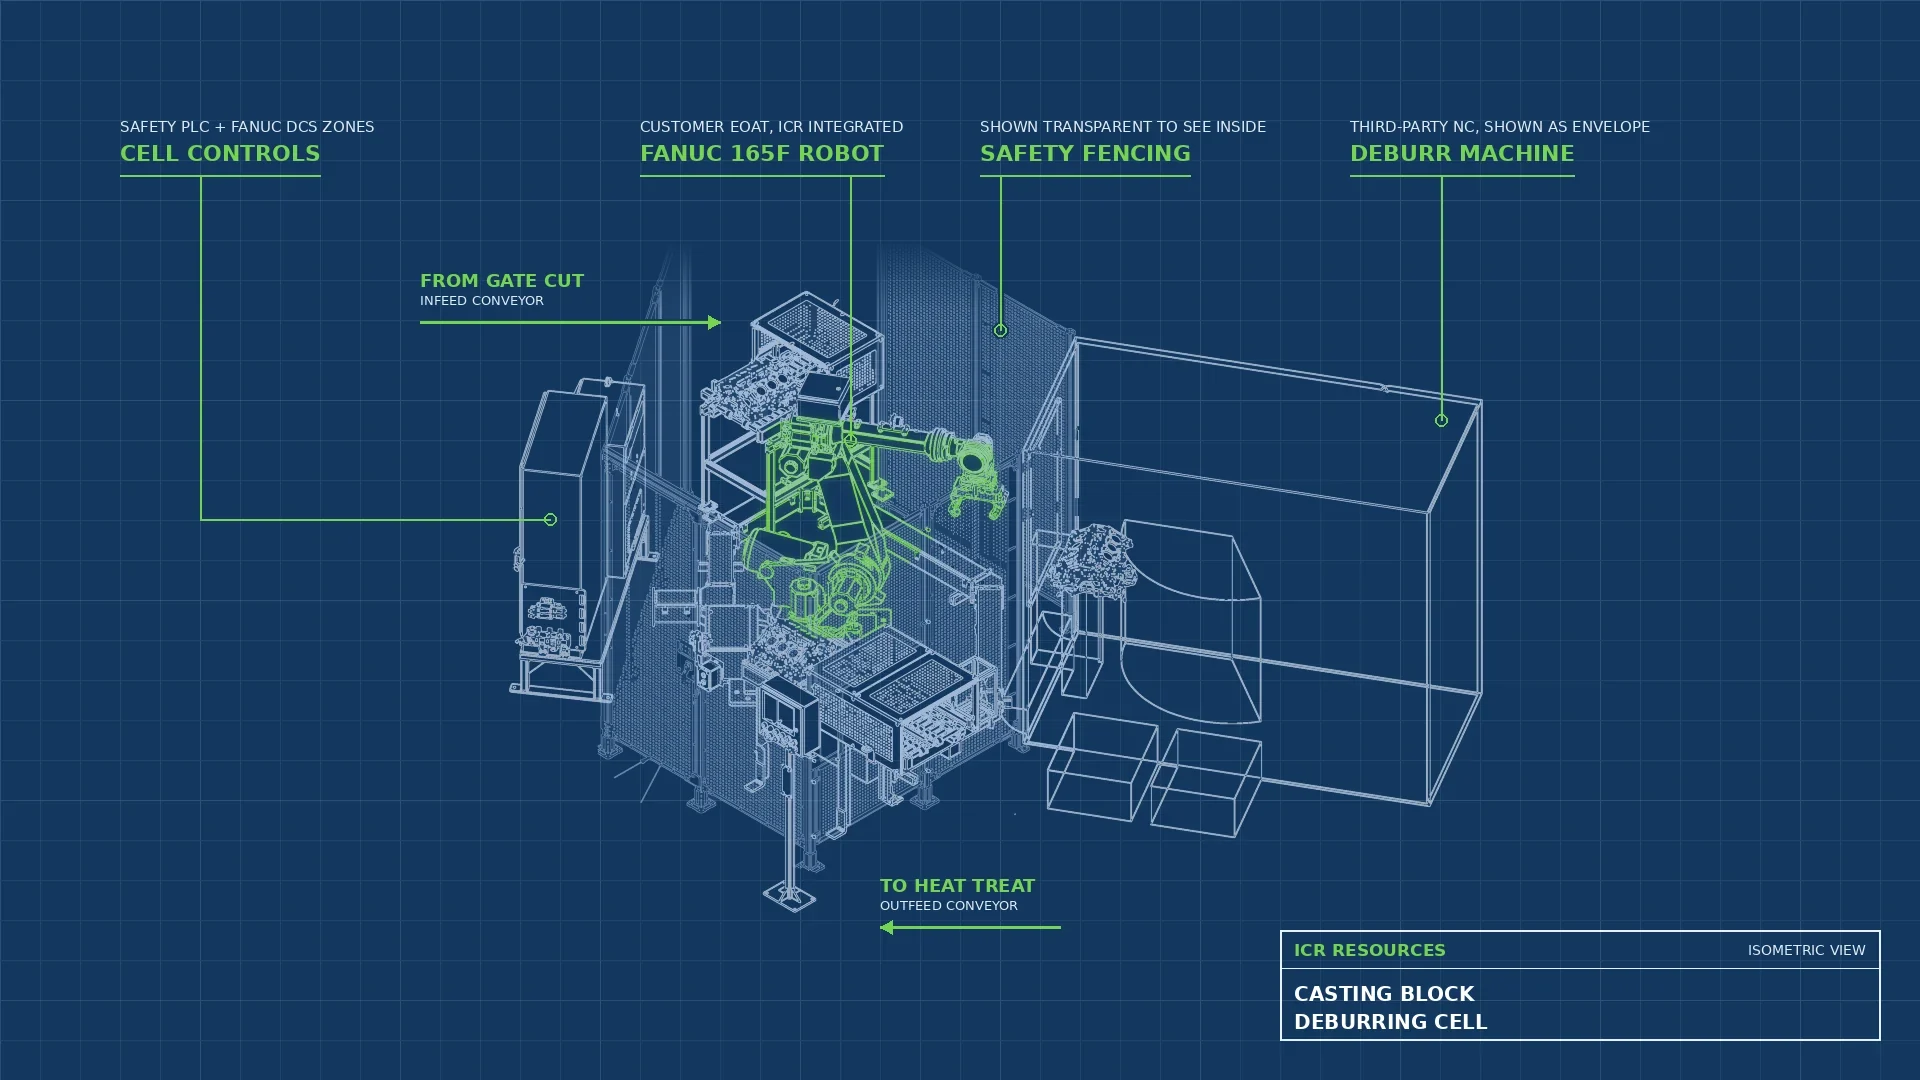
Casting blocks leaving the gate cut process had to be deburred before heat treatment. The customer had selected a third-party NC deburr machine and wanted to keep its existing conveyors, so the job was to tie it all together: move each heavy block from the infeed into the machine and back out toward heat treat, every cycle, without a person in the loop. Every block also had to stay traceable, and the cell had to keep team members out of the robot’s reach while still letting maintenance work safely.
Key Requirements
Receive blocks from the gate cut infeed conveyor
Load and unload a third-party NC deburr machine
Deliver deburred blocks toward heat treat
Read each block’s barcode for traceability
Rework and reuse existing customer conveyors
Keep personnel out of the robot envelope
The ICR Solution
ICR engineered a turnkey deburring cell around a FANUC 165F robot. ICR reworked the customer’s existing infeed and outfeed conveyors to present and receive blocks, and the robot, running customer-provided end-of-arm tooling, picks each block from the infeed, loads the deburr machine, then unloads it to the outfeed bound for heat treat. A barcode reader identifies every block for traceability. Safety is layered: perimeter fencing with a cell door and emergency release, Keyence light curtains, a safety PLC, FANUC DCS zones that limit where the robot can reach, and interlocks with the deburr machine and plant line. ICR built the control panel, HMI station and pneumatics, and programmed the cell.
Equipment & Technology
FANUC 165F robot (R-2000 class) with DCS safety zones
Customer-provided end-of-arm tooling
Reworked infeed and outfeed conveyors
Barcode reader and traceability station
Keyence GL-R light curtains and safety PLC
Cell control panel, HMI display and stand, pneumatics
Perimeter fencing with cell door, emergency release and teach key
Scope of Work
Up-Front Engineering
Mechanical Design
Conveyor Rework
Controls Design
Panel Build
Robot Integration
Safety System Design
PLC & Robot Programming
Installation
Commissioning
Results
Casting blocks now move from gate cut through deburr to heat treat with no manual handling. The robot keeps the deburr machine loaded around the clock, every block is read and tracked, and team members stay outside the hazard zone, with light curtains, DCS zones and interlocks guarding every entry point. Reusing the existing conveyors kept the footprint tight and the changeover short.