The customer’s low-pressure casting machines were worn out, and replacing them would have meant a major reinvestment. Rebuilding was the better path, but it meant locating and procuring hard-to-source parts, matching the OEM’s original design intent and countermeasuring the problems the machines had developed in service, so the rebuilt equipment would perform as a next-generation solution rather than a patched one.
Key Requirements
Rebuild to OEM design intent
Locate and procure hard-to-source parts
Countermeasure known failure points
Every cooling circuit: min. 10 LPM at 0.6 MPa
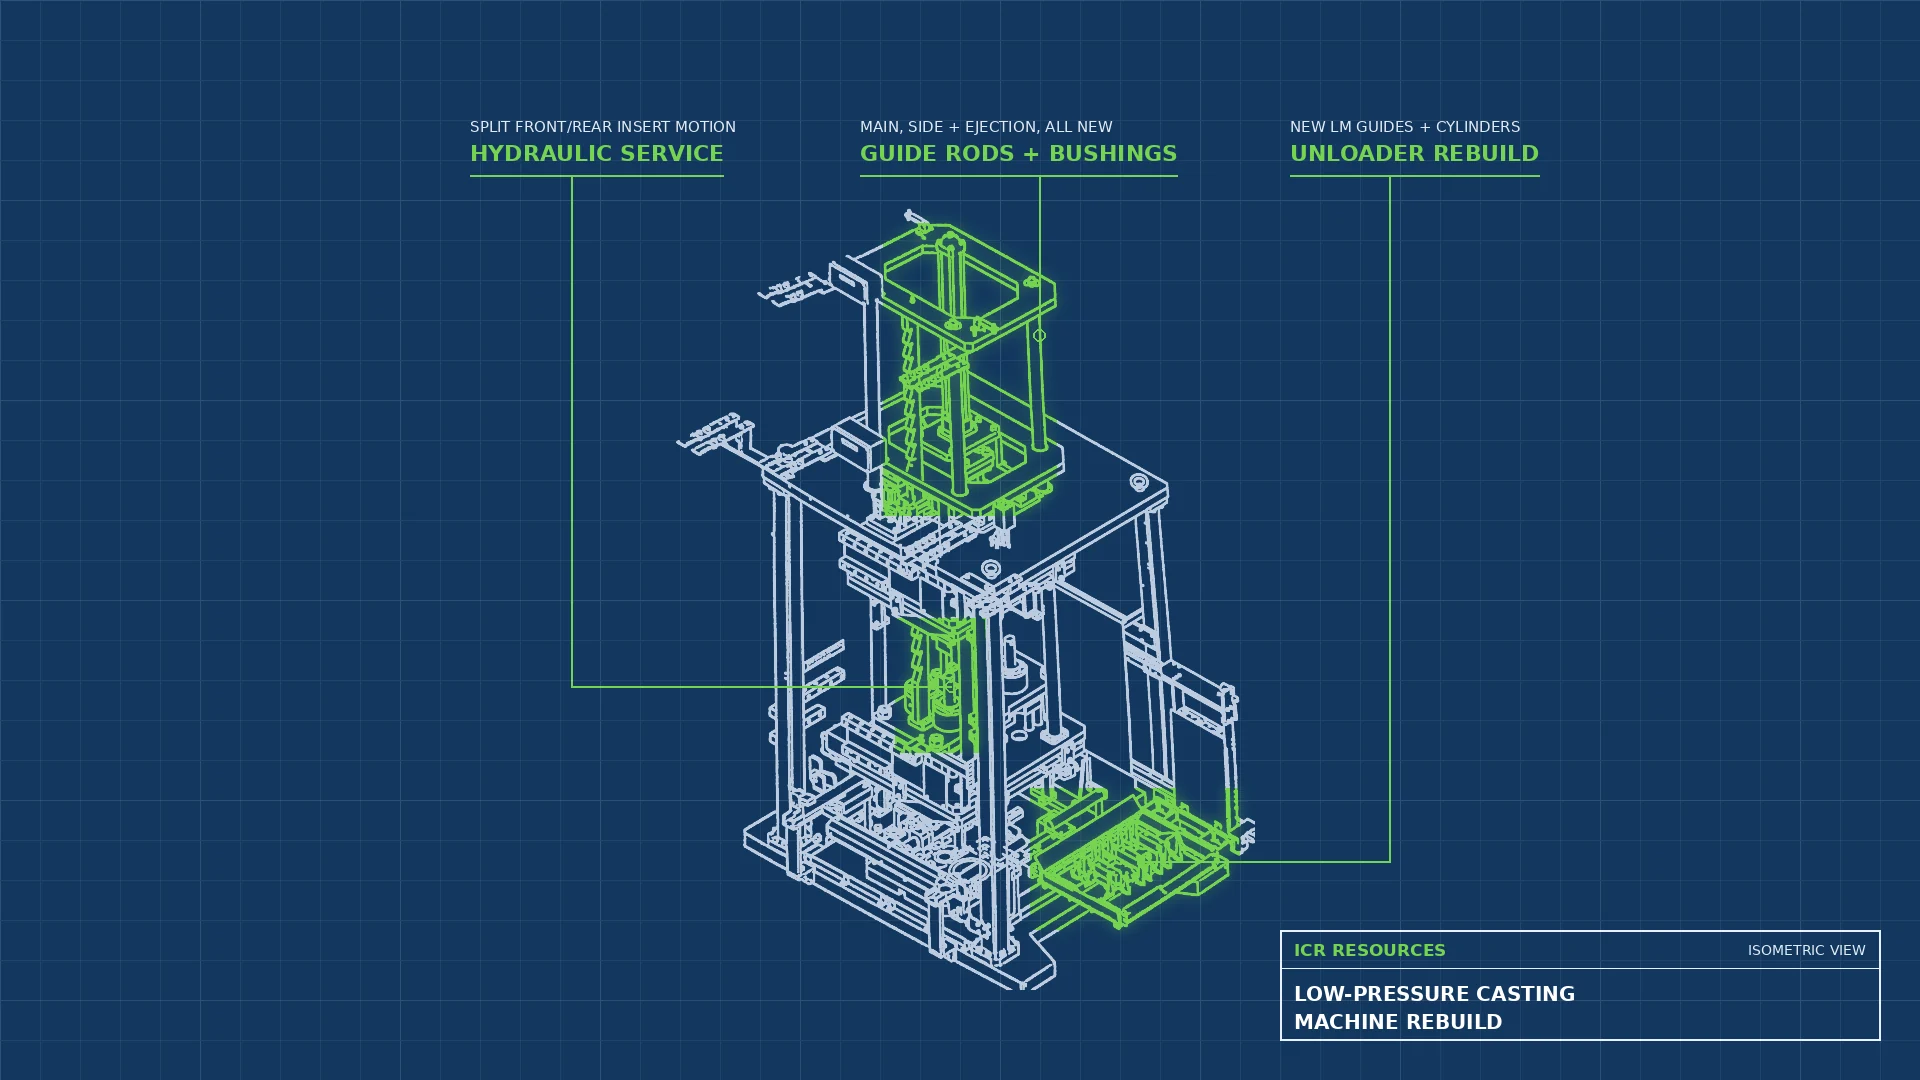
Service hydraulics and split front/rear insert motion
Modernize PLC and HMI to a 25 kA SCCR
Dry cycle at 35 seconds
The ICR Solution
ICR completed a casting machine rebuild on 26 machines, each one from the base up. Every guide rod and bushing (main, side, front, rear and ejection) was replaced, along with the ejection cylinder, split collar, stainless heat shields, die and base clamps, pushers and the fall-prevention pawl, springs and bushings. The unloader was rebuilt on new trays, LM guide rails and cylinders. The cooling system was flushed, leaks and faulty valves fixed, check valves added at the die entrance and every circuit flow-tested to 10 LPM at 0.6 MPa, with flow meters verified to ±0.5 LPM and all eight thermocouples replaced. A new hydraulic manifold split front and rear insert motion. Controls moved to a current-generation PLC and HMI with new master valves and a 25 kA SCCR, programmed to match the plant’s newest machines.
Equipment & Technology
Current-generation PLC and touchscreen HMI
New pneumatic master valves
Hydraulic manifold, pressure-reducing valves and 16 MPa gauges
Precision guide rods and bushings (main, side, front, rear, ejection)
Replacement ejection cylinder and stainless heat shields
LM guide rails and new cylinders for the unloader
Cooling check valves, flow controls and 8 thermocouples
Touch-start operator buttons
25 kA SCCR panel hardware
Scope of Work
Machine Assessment
Parts Sourcing and Procurement
Mechanical Rebuild
Hydraulic Service
Cooling System Overhaul
Controls Modernization
PLC/HMI Programming
Testing and Commissioning
Results
Rebuilding 26 machines saved the customer more than $1 million compared with buying new equipment, and the machines returned to production with known failure points countermeasured rather than simply replaced. Every cooling circuit was verified to spec, the hydraulics run leak-free, and the modernized controls match the plant’s newest machines, giving maintenance one standard to support and machines ready for 24/7 high-volume production.