The line feed relied on a belt-driven live roller conveyor whose rubber drive bands kept failing. The product was a heavy tray carrying 60 parts, and its irregular shape made transfer across band-connected rollers unreliable: rollers slipped, trays stalled and the line starved. The plant needed a robust conveyor that would move these trays to the pick station and return the empties without constant maintenance, and be installed with minimal disruption.
Key Requirements
Move heavy 60-part trays reliably
Handle an irregular tray footprint across every transfer
Supply lane to the pick station plus an empty-tray return lane
Positive drive with no slipping bands
Tray and part confirmation in every zone
Fully commissioned before shipping; installed in minutes
The ICR Solution
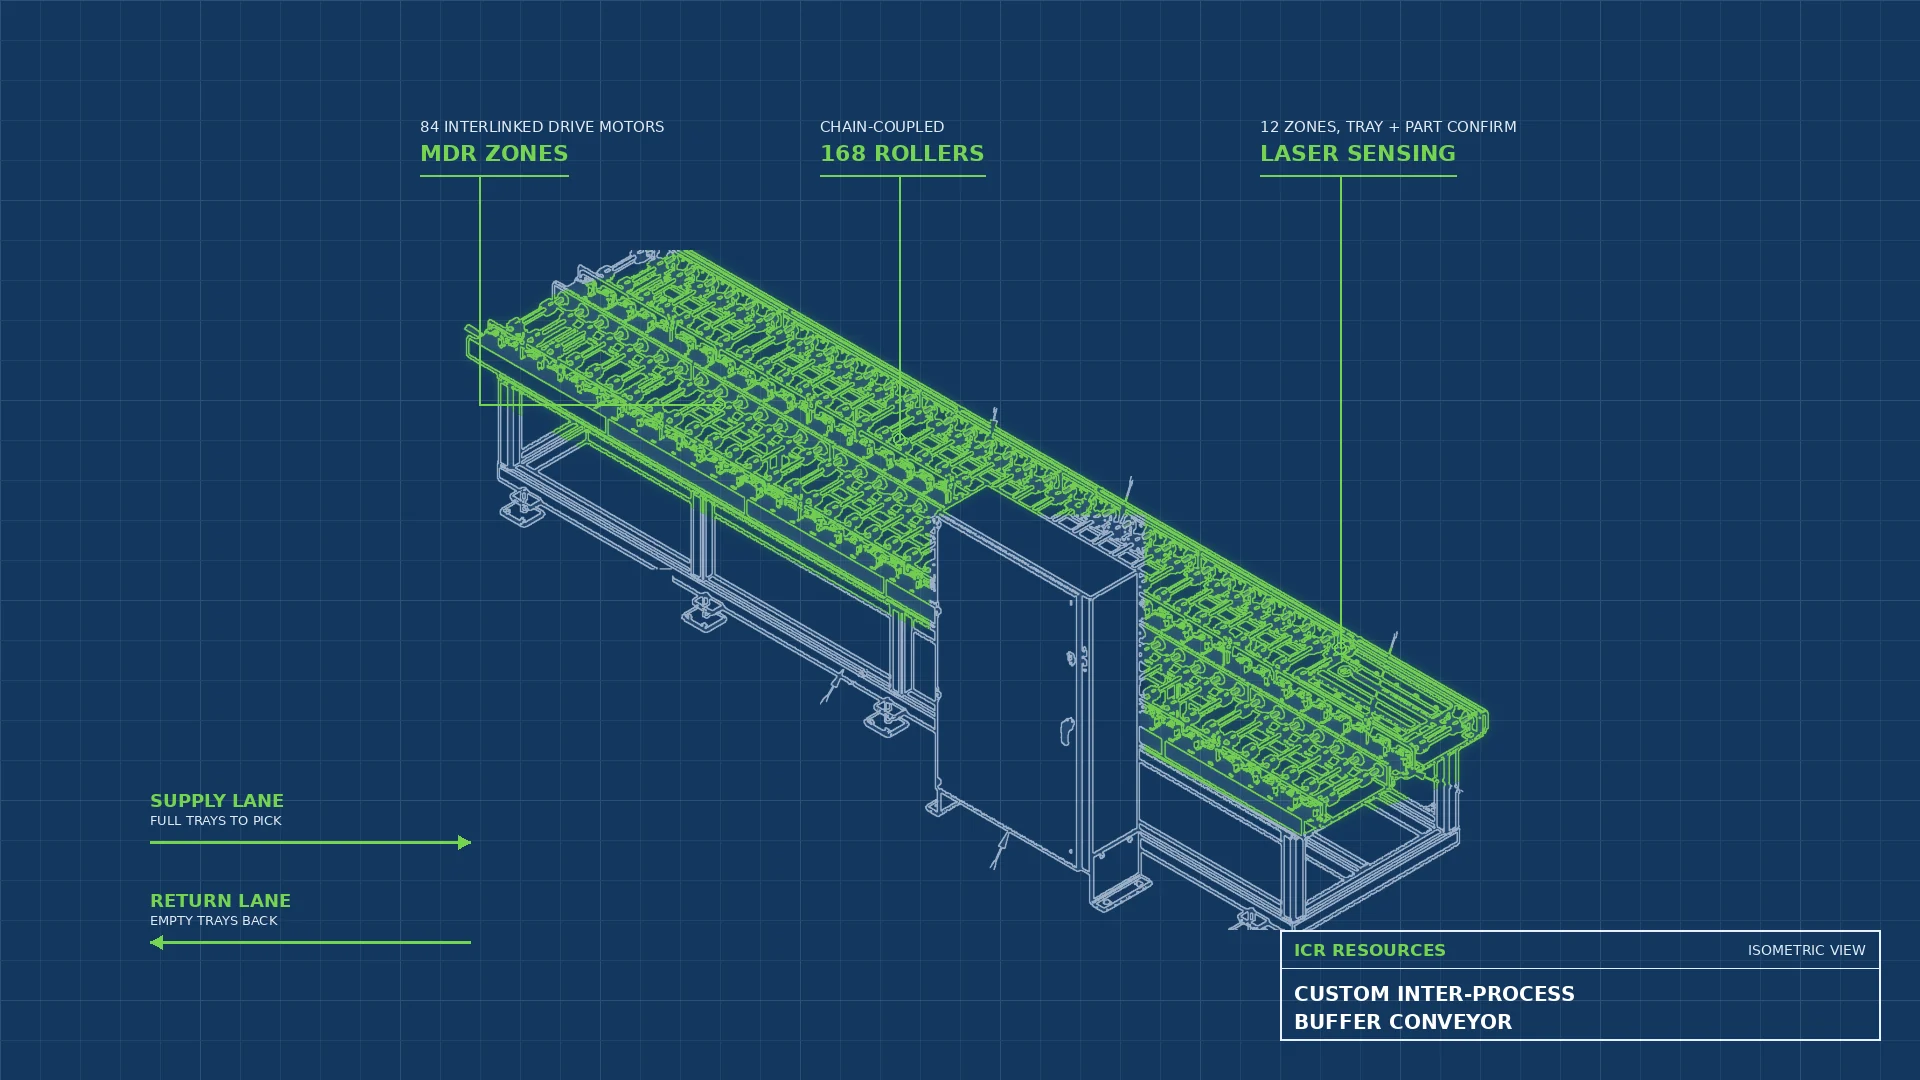
ICR replaced the band-driven design with a custom buffer conveyor built on motor-driven rollers (MDR). In every zone the drive motors are interlinked with the rollers by roller chain, so each roller is positively driven and a heavy, irregular tray keeps traction from one zone to the next. The conveyor runs as two six-zone lanes, a supply lane feeding full trays to the pick station and a return lane bringing empties back, with 84 drive motors turning 168 rollers. Keyence laser sensors confirm the tray and part in every zone, and the PLC manages each zone-to-zone transfer and the handshake with the pick conveyor. ICR fully commissioned the conveyor in its own facility, so installation took minutes.
The MDR line feed conveyor runs at 98% efficiency, replacing a band-driven conveyor that was a constant source of stalls and maintenance. Positive roller-chain drive keeps heavy, irregular trays moving through every transfer, and laser confirmation in each zone stops problems before they reach the pick station. Because ICR fully commissioned it before shipping, the conveyor was installed and running in minutes.