A packaging plant ran three conveyor lines on live roller drives, with rollers linked by rubber bands. The bands stretched and slipped, so rollers stalled, cartons hesitated and the lines lost throughput, while the bands themselves needed constant replacement. Product pushed against product, and the lines ran even when empty. The plant wanted positive drive, zoned accumulation and easier maintenance without replacing the conveyor frames.
Key Requirements
Convert three existing lines in place
Reuse existing conveyor frames
Zoned, zero-pressure accumulation
Run rollers only when product is present
Networked zone control
Minimize line downtime
The ICR Solution
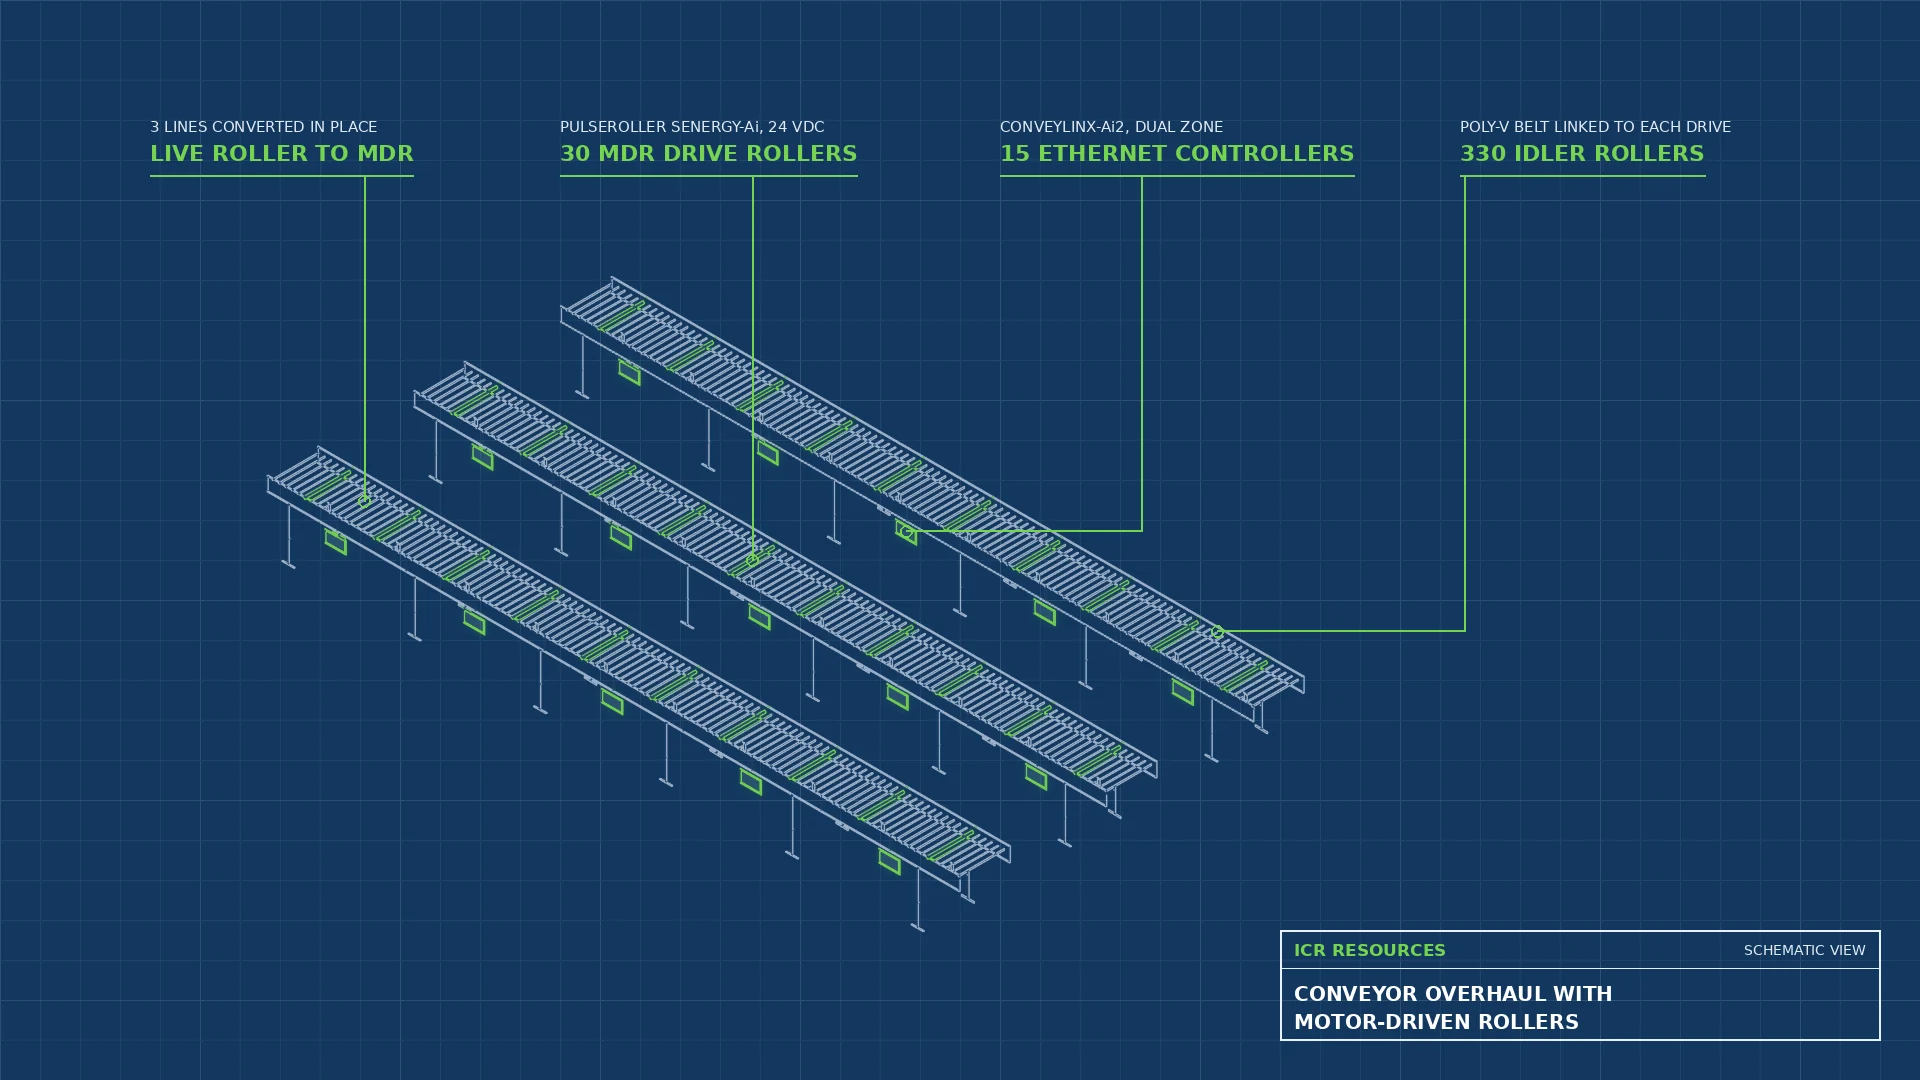
ICR surveyed each lane, then converted all three lines in place from live roller to motor-driven rollers (MDR). Each line was divided into 10 zones, each powered by a Pulseroller Senergy-Ai 24 VDC drive roller tied to its idler rollers by a timing-belt interconnection that does not slip like the old rubber bands, with 110 rollers per line. Five ConveyLinx-Ai2 dual-zone Ethernet controllers per line run the zones with built-in zero-pressure accumulation, using a photo-eye at every zone. Six 24 VDC power supplies per line feed the drives. ICR handled the conduit, wiring, networking and startup on site.
330 idler rollers with timing-belt interconnection
15 ConveyLinx-Ai2 dual-zone Ethernet controllers
30 zone photo-eye kits
18 MDR 24 VDC power supplies
Ethernet switches, sealtight conduit and M8 cabling
Scope of Work
Site Survey
Controls Design
Procurement
Mechanical Conversion
On-Site Wiring & Networking
Configuration
Startup
Results
All three lines now run at 99.5% efficiency on 30 zoned MDR drives. The timing-belt interconnection ends the roller slip that came with rubber bands, rollers turn only when product is in the zone, and cartons accumulate without pressure. Band replacement is gone, every zone reports on the Ethernet network, and a failed drive roller is a quick swap. The existing frames were reused, keeping the conversion fast.